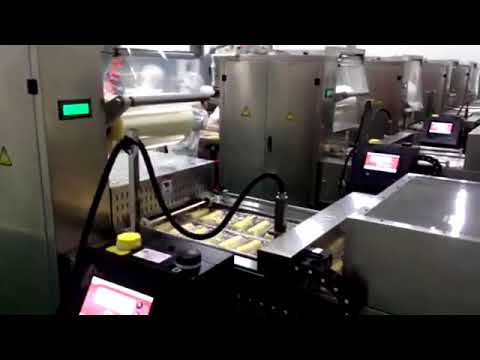
Showing posts with label food packing machine. Show all posts

Wednesday, July 11, 2018

Opinions regarding food waste in packaging process

Food is one of and most necessary needs for human. Until today, there are almost 1 billion people suffering shortage of food. So any kind of food waste is 100% unacceptable, and should thus be avoided.
A study from The Food and Agriculture Organization of the United Nations shows that about one-third of food produced for human consumption is lost or wasted in the world, which is about 1.3 billion tons per year. Food is lost or wasted throughout the whole supply chain, from the starting of agricultural production down to household consumption. According to the U.S. EPA, more than 38 million tons of food waste occurred in stateside in 2014, with only 5.1% diverted for composting.
In Canada, about $31 billion worth of food became landfills or composters each year with 47% of food waste happening at home (Value Chain Management International, 2014 report).
There are many initiatives around the world to address the issue of food waste in food packaging production. In 2015, the USDA and EPA announced a national food waste reduction goal, calling for a 50% reduction by 2030. The United Nations is adopting a similar objective as part of their new Sustainable Development Goals. France banned food waste, forcing supermarkets to sign agreements with charities so no edible food ends up in the trash. Italy’s Senate has passed a law that makes donating food easier for businesses and offers tax credits to supermarkets and farmers who donate. There is a proposal for a National Food Waste Reduction Strategy in Canada.
To efficiently reduce food waste, companies can start their food waste initiative by creating a waste reduction strategy to measure the impact of package use on the shelf life of their products. According to the plan, they can optimize the packing conditions, package format and materials to maximize shelf life and minimize food waste. The shipping container and pallet configuration should also be reviewed and optimized to minimize product damage.
Another efficient way to reduce food waste is the use of barrier packaging, but that means higher costs in packaging. Without using of barrier packaging, the quality of the food products may be compromised and shelf life shortened, so companies need to weigh the risk of dissatisfied consumers and loss revenue due to unsold products. It’s kind of dilemma, the best way is to perform a Life Cycle Assessment, which measures the environmental impacts of the package through the entire life cycle from production, usage to disposal. This can be a long and expensive endeavour.
Packaging can extend product shelf life so as to prevent food waste. It’s still a long way to address the food waste problem. The food packaging industry must balance consumer demands for sustainable packaging with demands for convenience, performance, appearance and cost. A quality package should protect and preserve the product and deliver it safely to the consumer.
Professional food packing machine manufacturer: Shandong Kangbeite Food Packaging Machinery Co.,Ltd, www.kbtfoodpack.com

Sunday, June 24, 2018

Common glitches in usage of chamber vacuum packing machines

Chamber vacuum packing machines are designed for home kitchen and small scale business. Both double chamber vacuum packing machine and single chamber vacuum packing machine are widely used by individual person or factory.
Machines always bump into breakdowns,  some are vital while some are just glitches that we can fix by ourselves.
In the following contents, I have a list of glitches and easy solve methods that i want to let you know. ( only for chamber vacuum packing machines)
Problem No.1 : Machine’s not working after chamber lid is pressed.
Reason analysis & Solve:
  • Fuse wire is broken  ———– Change fuse wire
  • Bad connection of microswitch ——– Adjust the switch chips
  • Bad power socket connection
  • Power voltage insufficient
  • Vacuum time set to 0 which is wrong ———reset vacuum time
Problem No.2: Power indicator light doesn’t work
  • Bad connection of power switch ——- replace the switch
  • Indicator light broken ——– replace the indicator light
Problem No.3: Vacuum pump is rotating without vacuuming
  • Press the chamber lid harder
  • The motor reverses —— exchange the power wire
  • Check and fix the gas route
  • Check and fix or replace magnetic valve
Problem No.4: Vacuum degree too low
  • Check somewhere with air leak problem: pipes joints; vacuum pump, vacuum meter, magnetic valve
  • Vacuum meter broken
  • Bag opening too little for air flow
Problem No.5: Fuse wire broken frequently
  • Too  high oil viscosity —- replace oil with appropriate viscosity
  • Environment temperature too low —– turn the machine on and warm up for a while
  • Drain vacuum pump oil to standard height
  • Check if the air draining filter is blocked
  • Short circuit in the electric circle

How to choose the right vacuum packing machine for your business

There are many varieties of vacuum packing machines in the market, which are widely used in household chicken and industrial level food factories.We will talk about small scale vacuum packer for chicken use a the other time, in this article, we are going to talk about the vacuum packaging machine for food factories only.
Firstly, i’d like to give a brief introduction of vacuum packing machine.
Before that, we need to know what is vacuum packing. Simply put ( Quote from Wikipedia:) Vacuum packing is a method of packaging that removes air from the package prior to sealing.
This method involves (manually or automatically) placing items in a plastic film package, removing air from inside, and sealing the package. (Alternative Modified air packaging is part of the process)
So vacuum packing machine is a series of machines designed to complete the process in good conditions.
Vacuum Packing Machine main varieties (Sort by packing efficiency lower to higher):
So now we have the ultimate question, how should I choose the right vacuum packing machine for my business?It’s very simple,  you only need to know 2 things: Know your products to pack, Know the machine to do the packing process. It’s easily said than done, so i’ll explain in the following details.
  1. Check the vacuum pump working on the vacuum packing machine. Vacuum pump is the heart of a VACUUM packing machine. It determines the whole quality of the machine, and vacuum degree, vacuuming speed, packing efficiency, everything. We use the world famous BUSCH vacuum pump. which price is several times more expensive than the lower quality vacuum pumps.
  2. PLC system and electric components. I call the PLC as the brain, and electric components as the nerve system of the whole vacuum packaging machine. These parts need top quality, high compatibility, and most advanced technology. Usually in a good quality food vacuum packing machine, the following famous brand components are adopted: Mitsubishi, Siemens, Schneider.
  3. The main frame and structure should be strong enough and comply with safety&hygienic standards. Main materials for a good quality vacuum packing machine: Food grade SUS304 stainless steel, Magaluma main shaft, Acrylic safety cover for main processes. Whole machine should comply with CE certification and all necessary certifications.
  4. Well designed machine structure, with all necessary functions and compatibility for extra functions in further future.
  5. Concern about the factory’s after-sale service. Especially for international trade, whether the factory can provide overseas service is very important.
  6. Don’t simply make decisions the sales presents talks and the appearance of the machine. You better visit the factory with a technician on your side who can easily judge the quality of the machine.
  7. You should know your product: When communicating with the sales representative, you always want them to give an ideal solution for your business as soon as possible. So you should tell them the specification of your products – food or non-food, liquid or powder or solid products, the sizes, the size of your packages, material of the packing bags, the packing method,  your expected packing efficiency, if you need extra functions, if you need the machine in restricted sizes to adapt to your working place, etc
With the above details, you have most of the points to pick the right vacuum packaging machine for your business.
If you are purchasing the machine from abroad, please noted that additional fees will occur, and you need to know the process of importing a product, or you can easily find an import agent from nearby to help you with the work.